Donaldson targets dust challenges with SSG+ air cleaner
Simple solutions can provide remarkable results
Mining equipment operates in some of the harshest and most dust-laden environments in the world. For modern high-horsepower diesel engines, protecting the air intake system is critical to engine performance, reliability and service life.
A modern diesel engine can consume up to 20,000 litres of heavily contaminated air for every litre of diesel fuel burned. On large haul trucks and other heavy mining equipment, that places enormous demands on the engine air filtration system.
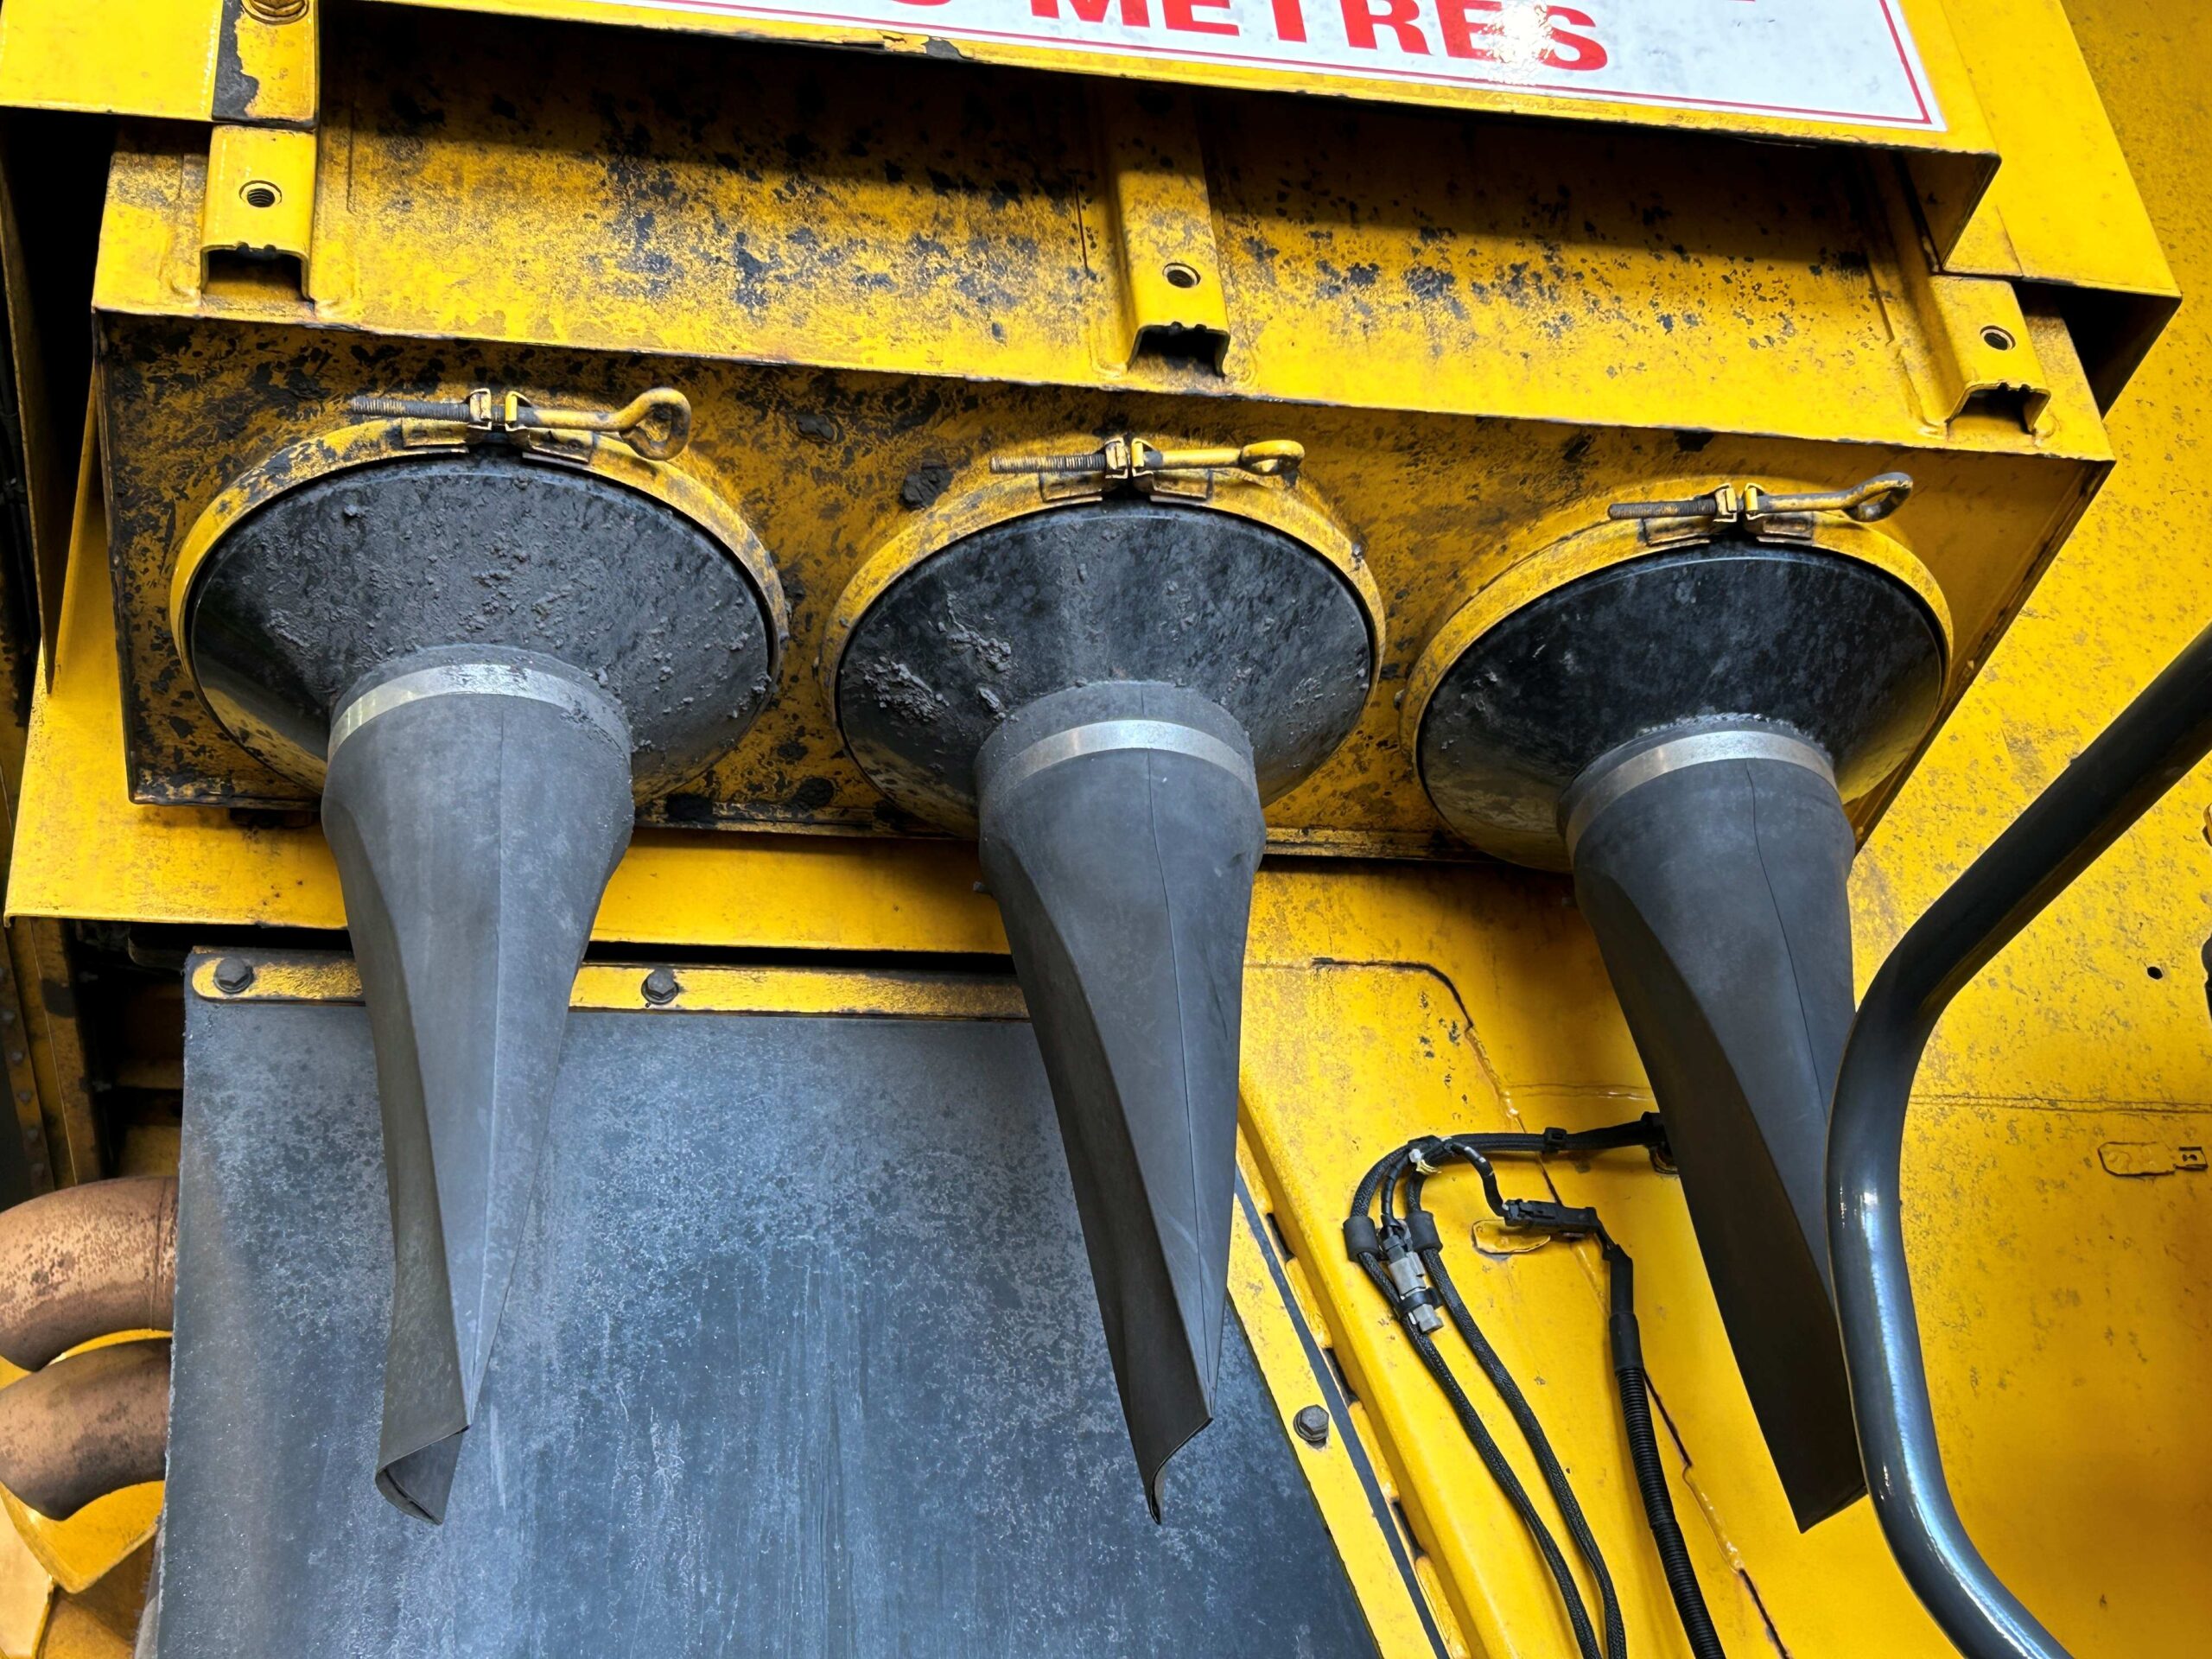
Donaldson Filtration Solutions designed the SSG+ Donaclone™ air cleaner, a high-capacity filtration system engineered specifically for these demanding conditions. Building on Donaldson’s proven SSG technology, the SSG+ combines advanced two-stage filtration with integrated rain protection, safety filtration and Donaldson’s Trickle Valve dust evacuation system as standard. The first stage uses inertial pre-cleaning to separate a significant proportion of heavier dust before it reaches the primary filter. This separated dust falls into the lower dust cups, where it can be evacuated from the housing.

The result is a factory-integrated solution designed not only to protect the engine, but also to address one of the persistent maintenance challenges experienced on mine sites; dust caking and ineffective dust evacuation.
Under laboratory conditions, a dual SSG RadialSeal™ housing can separate and filter more than 200 kg of test dust before reaching the maximum allowable intake restriction commonly associated with modern engines.
Dust characteristics vary considerably between operations, and static, moisture and environmental conditions can cause fine material to cling to internal surfaces rather than evacuate cleanly. Water introduced during vehicle wash-downs can make the problem significantly worse.
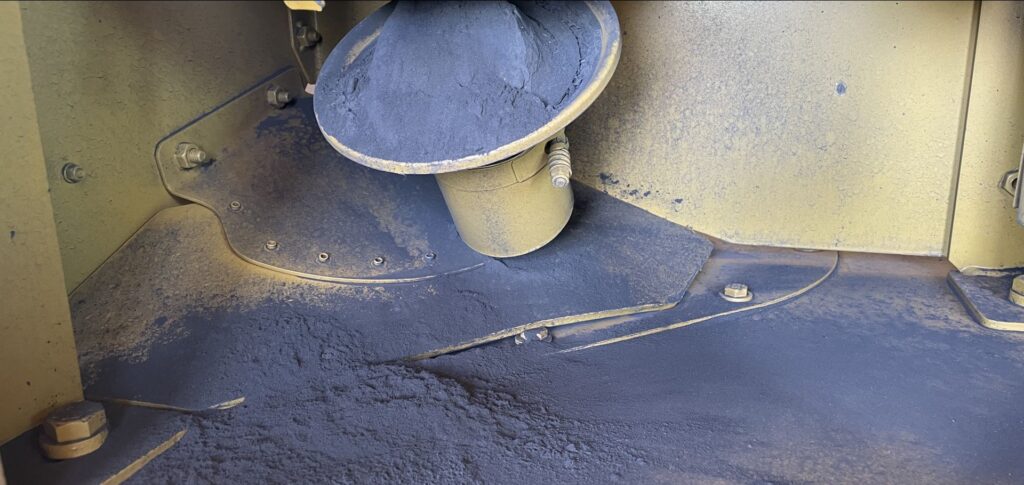
When fine dust and water combine, the resulting material can form a dense mud that dries and hardens inside the lower section of the air cleaner. Once this occurs, dust evacuation can be compromised and the effectiveness of the pre-cleaning system reduced.
The consequences can include shortened primary filter life, increased restriction events and additional labour-intensive air intake maintenance.
Australian mining operations are increasingly focused on workshop hygiene and reducing personnel exposure to nuisance dust. However, some maintenance practices introduced to control dust exposure can unintentionally contribute to air cleaner problems.
Sites have trialled a range of approaches to improve dust evacuation, including earth straps, scavenge fans, reverse-pulse systems, alternative pre-cleaners and changes to vacuator valve configurations.
Wash-down practices can also introduce additional challenges. Opening dust cups before entering a wash pad or using high-pressure water to clean lower air cleaner bodies can expose pre-cleaner tubes to significant quantities of water.
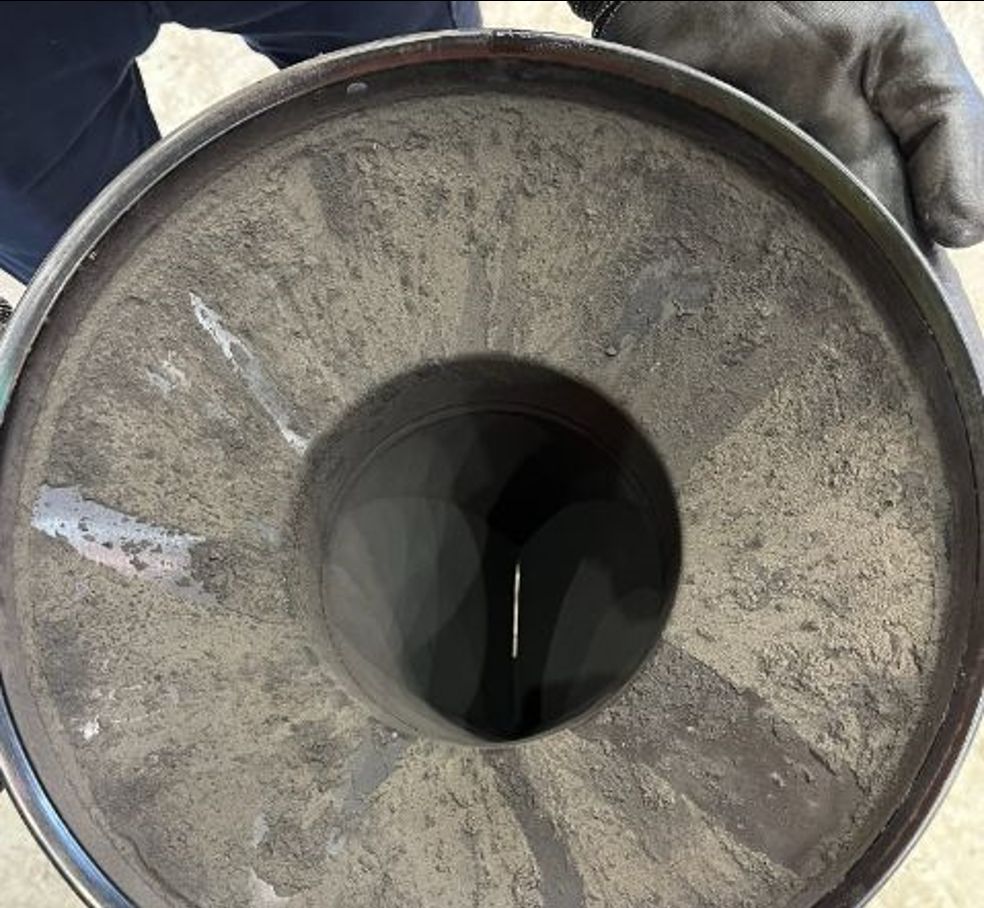
With mining fleets under pressure to maximise availability, equipment may return to service before the air cleaner has had sufficient time to dry. The combination of residual moisture and fine mine dust can then accelerate caking, restricting the system’s ability to evacuate separated dust.
This creates a cycle in which reduced pre-cleaning efficiency increases the dust load on the primary filter, potentially shortening usable element life and creating high restriction events.
Donaldson Australia worked with mining customers to investigate alternative dust evacuation methods that could address these real-world challenges without adding unnecessary maintenance complexity.
Rather than relying on the conventional quick-release dust cup arrangement, the Trickle Valve assembly uses a tapered fixed cup with an integrated 6-inch valve port. This eliminates the additional gasket and conventional 3-inch vacuator valve arrangement previously used at the base of the housing. The pliable 6-inch injection-moulded Trickle Valve is designed to support effective dust evacuation while helping prevent water ingress during vehicle wash-downs.
The Trickle Valve underwent extensive testing at Donaldson’s Minnesota air laboratories, followed by field trials across several Australian mine sites. These trials confirmed the laboratory findings and demonstrated that the system could remain in position and operate effectively for more than 8,000 hours without routine labour intervention. For mine operators, this has the potential to transform what was previously a regular maintenance activity into an annual inspection task.
When combined with appropriate air cleaner maintenance practices, the SSG+ and Trickle Valve are designed to help minimise dust caking, maintain effective pre-cleaning, prolong primary filter life and reduce high-restriction events. Fewer interventions also mean fewer maintenance steps and less personnel interaction with accumulated nuisance dust.
Donaldson will be exhibiting at IMARC on Stand T35, where visitors can see the SSG+ Donaclone™ air cleaner and Trickle Valve system on display and speak directly with Donaldson filtration specialists.
Whether the objective is to simplify air cleaner maintenance, reduce dust-related servicing, lower operating costs or improve equipment uptime, the Donaldson team can discuss how the Trickle Valve and SSG+ can deliver measurable benefits for your operation.