Tough connections for tough sites
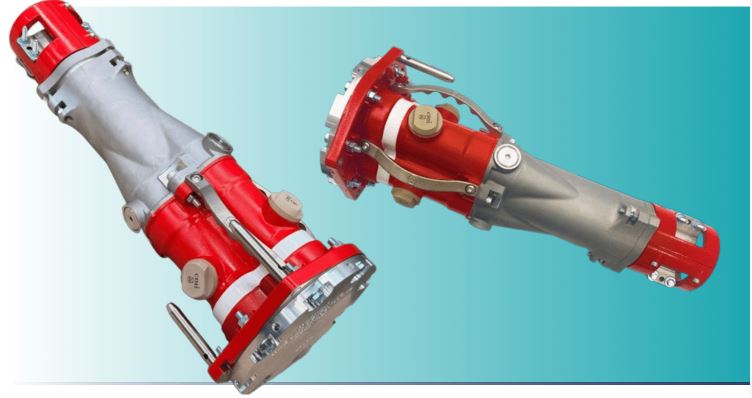
CMI Electricals’ Minto 800A 11kV Bolted Coupler Range
Reliable high-voltage power is critical to the productivity, safety, and performance of modern mining and tunnelling operations. In these environments, electrical infrastructure is exposed to constant vibration, dust, moisture, mechanical stress, and frequent handling. For engineers and maintenance teams, the priority is making sure critical connections remain safe, stable, and straightforward to maintain over the long term.
Trailing and feeder cable connections are some of the most heavily worked components in any high-voltage distribution network. They’re regularly moved, flexed, and subjected to mechanical loading, which means they can quickly become a source of downtime if they’re not properly designed. Despite this, they’re often still treated as consumables instead of as critical parts of the electrical system.
CMI Electricals’ 800A 11kV Bolted Coupler Range has been developed specifically with these challenges in mind. Built for mining and tunnelling applications, it provides a reliable solution for trailing and feeder cable connections where performance and safety are essential.
The coupler is rated at 800A continuous current and has a verified short-circuit withstand rating of 13.5kA. This allows it to support high-demand applications such as distribution substations, pump stations, longwall mining systems, and tunnel boring machines (TBMs). These ratings give confidence that the coupler will perform reliably not only during normal operation but also under fault conditions.
A key part of the design is the bolted connection system, which maintains consistent contact pressure even with vibration and cable movement. This is particularly important for trailing cable applications, where repeated handling and mechanical stress can compromise contact integrity. By maintaining firm contact pressure, the design helps minimise heat build-up, reduce wear on contact surfaces, and prevent premature failures.
Safety has also been built into the design. Non-contact voltage test points are included across all three phases, allowing operators to confirm the presence or absence of voltage before handling equipment. This supports safer isolation procedures and reduces the risk of electrical incidents during maintenance or cable handling. Internally, the coupler uses phase segregation by earth. This reduces the likelihood of phase-to-phase faults and helps limit electrical interference within the system. As mines continue to adopt more automation, monitoring, and communication systems, maintaining a stable electrical environment across the network becomes increasingly important.
For insulation performance, PTFE phase insulators have been selected. PTFE offers excellent dielectric strength and strong resistance to electrical tracking, helping maintain insulation integrity in harsh conditions where dust, moisture, contamination, and temperature cycling are unavoidable. This contributes to long-term reliability and reduces the risk of insulation-related issues.
Installation and maintenance have been simplified by eliminating compound filling. Combined with an IP66/IP68-rated enclosure, the coupler provides strong protection against dust and water ingress without adding unnecessary complexity during installation. Removing compound filling also helps reduce the likelihood of installation errors and makes ongoing maintenance more straightforward.
Serviceability is another key consideration. Phase pins and pilot components can be replaced without full disassembly of the coupler, allowing maintenance teams to conduct targeted repairs quickly and efficiently. This reduces downtime, improves equipment availability, and minimises the need to hold complete spare units in stock.
Compatibility with cold-shrink terminations further improves installation efficiency. This allows for faster and more consistent cable preparation, helping standardise installation practices across crews and reduce variability in workmanship.
The range is available in a number of configurations to suit different site requirements. These include 4-bolt and 8-bolt designs, pilot and non-pilot versions, and a variety of cable clamp arrangements. This flexibility enables engineers to select a configuration that fits the specific application without compromising on performance or reliability.
Material selection has also been carefully considered to suit underground and surface mining conditions. The combination of a robust aluminium body, stainless steel hardware, and silver-plated copper current-carrying components provides strong mechanical performance, high conductivity, and resistance to corrosion. This helps ensure the coupler can withstand demanding operating environments over an extended service life.
In practice, long-term performance of connection systems is rarely limited by electrical ratings alone. More often, failures are driven by mechanical fatigue, insulation degradation, or components that are difficult to maintain effectively in the field. Addressing these factors is key to improving reliability and reducing unplanned outages.
The CMI Electrical 800A 11kV Bolted Coupler Range has been designed with these realities in mind. By combining solid mechanical design, integrated safety features, reliable insulation, and practical serviceability, it provides a connection solution that aligns with the day-to-day demands of mining and tunnelling operations.
For engineers and maintenance teams, this means a high-voltage connection system that is dependable, safer to work on, and easier to maintain. The result is better network reliability, reduced downtime, and greater confidence in the performance of critical electrical infrastructure across the life of the asset.
Now available through CMI Electrical
cmielectrical.com.au
1800 264 222